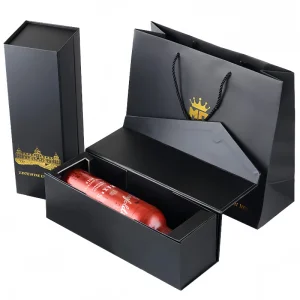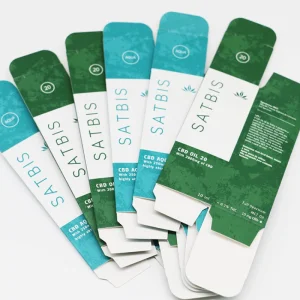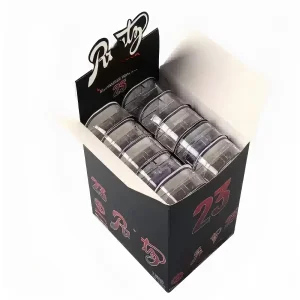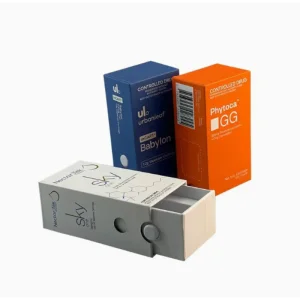
Since its establishment in 2017, Brightpack has evolved into a leading manufacturer specializing in premium custom packaging solutions for global markets. We combine functional design, high-quality materials, and advanced production to create packaging that elevates brand identity and meets international standards.
Our one-stop service covers every stage from design consultation, material selection, and custom printing to strict quality control, logistics coordination, and compliance support. Backed by a 2,000㎡ modern facility and a team of 100+ skilled professionals, we ensure precision, efficiency, and reliability in every order.
Whether you need luxury gift boxes, eco-friendly packaging, or industry-specific solutions, our commitment to innovation and customer satisfaction makes us your trusted partner for global packaging success.
Years Experience
Advanced Factories
m² Facility
Skilled Employees
As global enterprises look for cost-efficient yet premium packaging solutions, China's manufacturing ecosystem—specifically in advanced offset printing and lithography—has established an unmatched competitive edge. By integrating high-speed Heidelberg printing presses, computer-to-plate (CTP) technologies, and automated die-cutting workflows, manufacturers like Brightpack deliver precise color fidelity (Delta E < 2) and high-volume consistency that meets strict European and American retail benchmarks.
Navigating cross-border procurement requires rigorous adherence to international regulatory frameworks. Our compliance-first design system incorporates global standards such as EU REACH for chemical safety in packaging inks, US FDA 21CFR for food-contact paper containers, and IPPC ISPM 15 standards for wooden packaging components. By preemptively mitigating 90% of customs compliance risks at the pre-press design phase, we ensure frictionless logistics and border clearance.
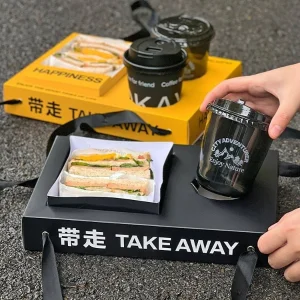
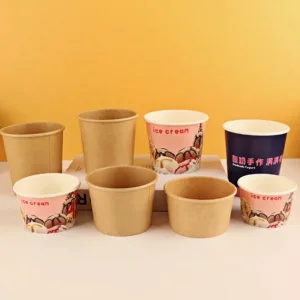
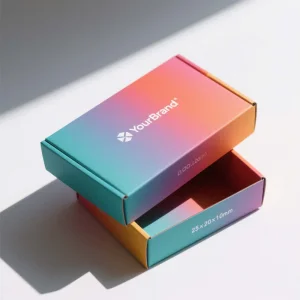
Lithographic printing and offset packaging are transitioning towards smart packaging and sustainable materials. Key application scenarios span across luxury cosmetics, consumer electronics mailer boxes, biodegradable food service trays, and specialty beverage packaging. Trend analysis reveals a 42% year-over-year surge in demand for recyclable paper substrates coupled with tactile surface treatments such as soft-touch lamination, holographic anti-counterfeiting foils, and embossed typography.


Specialized in export-oriented packaging design, studying regulations of 50+ target countries/regions to pre-resolve customs risks.

Backed by advanced die-cutting (tolerance ≤±0.5mm) and HD printing up to 1200dpi for complex structural designs.

From FSC-certified paper to VOC-free inks, undergoing 15 inspection checkpoints with a defect rate under 0.5%.

Offering 3-day rapid sampling and 7-day mass production with lean scheduling for global business expansion.
A: Offset printing (lithography) uses metal plates to transfer images onto rubber blankets and then printing surfaces. It is the most cost-effective and highest-quality method for medium to large production runs, offering superior color accuracy (Pantone matching) and sharpness at 1200+ DPI.
A: All our food-grade packaging materials utilize FSC-certified paper stock and VOC-free, food-safe vegetable inks compliant with US FDA 21CFR and EU food contact regulations, safeguarding your brand against regulatory liabilities.
A: For customized samples, we deliver within 3 days. For mass production runs (e.g., 10,000 to 100,000 units), our streamlined lean manufacturing schedule ensures completion within 7 to 12 days with 98% on-time global delivery.