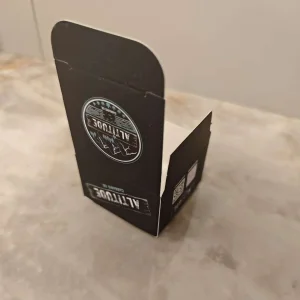
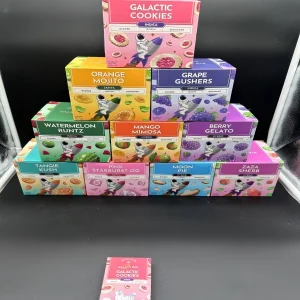
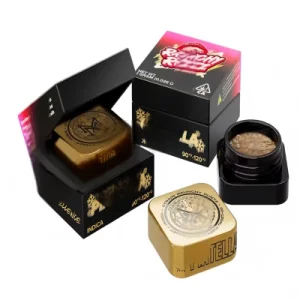
Since its establishment in 2017, Brightpack has evolved into a leading manufacturer specializing in premium custom packaging solutions for global markets. We combine functional design, high-quality materials, and advanced production to create packaging that elevates brand identity and meets international standards.
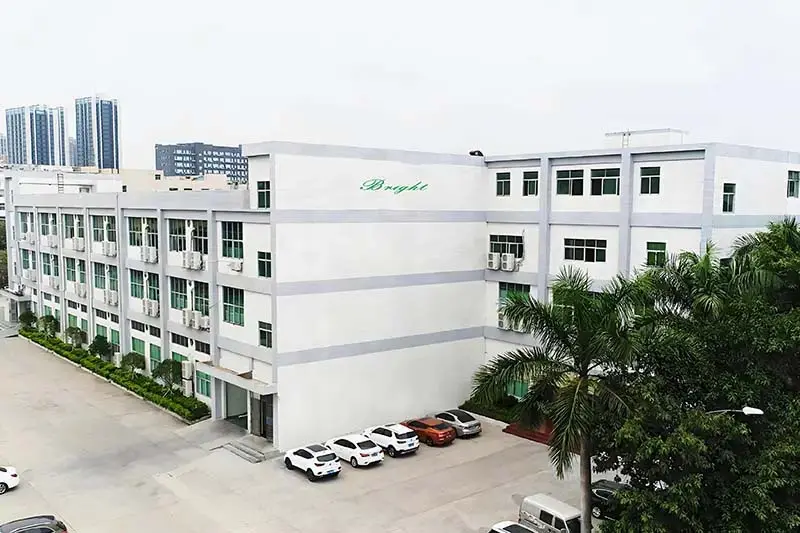
Our one-stop service covers every stage from design consultation, material selection, and custom printing to strict quality control, logistics coordination, and compliance support. Backed by a 2,000㎡ modern facility and a team of 100+ skilled professionals, we ensure precision, efficiency, and reliability in every order.
Whether you need luxury gift boxes, eco-friendly packaging, or industry-specific solutions, our commitment to innovation and customer satisfaction makes us your trusted partner for global packaging success.
Years
Factories
m²
Employees
In today's fast-paced global supply chain ecosystem, the demand for structural integrity and damage mitigation during transit has reached an all-time high. Corrugated boxes integrated with custom partitions (also known as dividers or grid inserts) represent the pinnacle of protective packaging engineering. Across e-commerce, electronics, pharmaceutical, and specialty beverage sectors, enterprises are shifting away from generic single-wall cartons toward precision-engineered partitioned corrugated containers. These systems isolate individual items, eliminate inter-product friction, and distribute compressive loads evenly across multi-tier stacking configurations.
As international trade volumes expand, logistics networks encounter severe mechanical stress points—ranging from automated sorting facility drops to long-haul maritime vibration. Utilizing OEM corrugated boxes with partitions significantly reduces return rates caused by transit damage, safeguarding brand reputation and optimizing bottom-line logistics expenditures.
The versatility of corrugated boxes with partitions makes them indispensable across diverse localized vertical markets:
Retail & E-commerce Fulfillment: Used heavily for shipping fragile glassware, artisanal cosmetics, and high-end vape or CBD cartridges (such as 510 cartridge packaging boxes). Partitions ensure that multi-item bundled orders remain immovably secured inside mailer boxes.
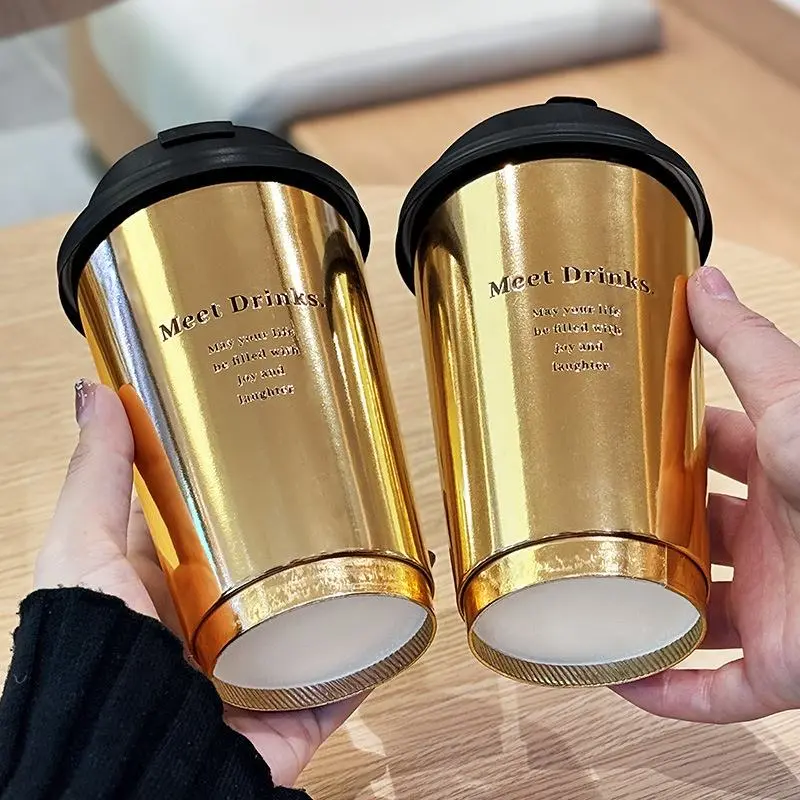
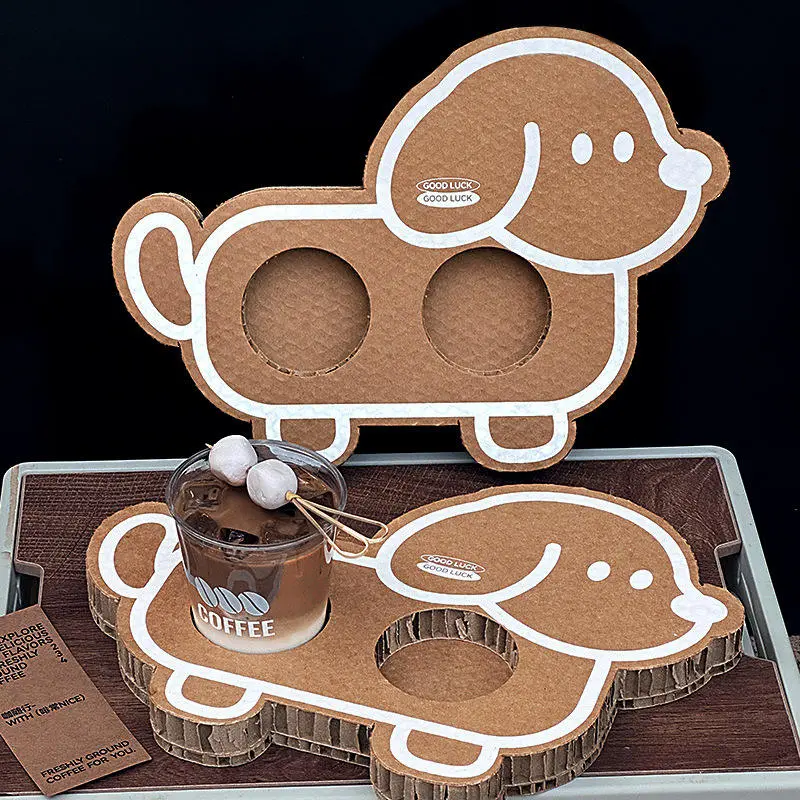
Food & Beverage Industry: Applied in custom display boxes and single coffee/tea cup holders, where corrugated partitions provide thermal insulation barriers and prevent liquid container displacement during delivery.
Industrial Component Storage: Automotive and electronic parts manufacturers utilize heavy-duty double-wall corrugated boxes with die-cut partitions to segregate sensitive metallic components, preventing scratching and electrostatic discharge accumulation during assembly line transit.
China's manufacturing ecosystem remains the undisputed powerhouse for bespoke corrugated packaging production. Leveraging integrated industrial clusters, top-tier packaging suppliers combine high-speed fluting laminators, automated die-cutting presses (tolerance ≤±0.5mm), and computer-aided structural design to deliver unmatched scalability.
Agile Production & Lean Scheduling: Modern factories maintain robust tiered raw material reserves (FSC-certified kraft paper, recycled fluting media), enabling rapid turnaround times—such as 3-day rapid prototyping and 7-day mass production for tight promotional deadlines.
Cost-to-Performance Ratio: Advanced automation minimizes labor overhead while maximizing output consistency. This structural efficiency allows global brands to procure premium-grade OEM corrugated boxes with partitions at highly competitive unit economics without sacrificing structural integrity.
The next decade of corrugated packaging engineering will witness a profound convergence with digital traceability and smart materials:
IoT & NFC Integration: Embedding RFID tags and Near Field Communication markers directly into corrugated partition flaps to facilitate real-time inventory tracking and anti-counterfeiting verification.
Nanotechnology Coatings: Developing hydrophobic and antimicrobial cellulose-based coatings that extend packaging lifespan in high-humidity export environments while remaining 100% repulpable and biodegradable.
Generative Structural Design: Utilizing AI-driven algorithms to simulate drop-test physics and optimize flute profiles (e.g., transitioning between A, B, C, E, and F flutes) to achieve ultimate lightweighting while maintaining maximum BCT (Box Compression Test) ratings.
Navigating international import regulations is a critical friction point for global brand owners. Brightpack’s compliance-first design system preemptively addresses complex regulatory frameworks across more than 50 target export jurisdictions:
Environmental Compliance: Adhering strictly to EU REACH directives concerning chemical substances in paper and board packaging, as well as US FDA 21 CFR standards for secondary food-contact packaging materials.
Phytosanitary Standards: Implementing rigorous ISPM 15 compliance protocols for any auxiliary wooden pallet components to guarantee frictionless customs clearance and eliminate border quarantine delays.
Q1: What are the primary advantages of adding partitions to corrugated boxes?
A1: Partitions create individual cells that absorb shock, prevent product-on-product collision, and drastically enhance the vertical stacking strength (BCT) of the outer container, making them ideal for fragile or multi-piece shipments.
Q2: Can I customize the dimensions and cell count of the corrugated partitions?
A2: Absolutely. As a direct OEM manufacturer, we engineer custom die-cut inserts tailored precisely to your product dimensions, whether you need a 4-cell, 12-cell, or 25-cell grid layout.
Q3: What is the standard minimum order quantity (MOQ) for custom printed corrugated boxes with partitions?
A3: We offer highly flexible production tiers to support both emerging brands and enterprise-scale rollouts, with low MOQs for digital print runs and highly scalable volume pricing for mass industrial orders.


Specialized in export - oriented packaging design, we’ve studied regulations of 50+ target countries/regions (e.g., EU REACH for packaging materials, US FDA 21CFR for food - contact items). For example, when handling wooden - component packaging, we strictly apply the IPPC marking process. By pre - resolving 90% of potential customs clearance risks in the design phase, we ensure smooth overseas shipping, saving you from costly delays.

Backed by advanced die - cutting (tolerance ≤±0.5mm) and HD printing (resolution up to 1200dpi) equipment, we master complex structures like auto - lock bottom folding boxes and luxury rigid boxes with lids. For high - end brands, our holographic anti - counterfeiting + embossing processes can boost brand perceived value by 35%, accurately translating your brand identity into packaging.

From sourcing FSC - certified paper to using VOC - free inks, we control every material. In finished product testing, we simulate 10+ transportation scenarios (ocean shipping vibration, air freight drop tests). Each batch goes through 15 inspection checkpoints, achieving a defect rate of less than 0.5%, far below the industry average of 3%.

With a 2,000㎡ owned factory and a 3 - tier outsourcing network, we offer:
Small batches: 3 - day sampling, 7 - day mass production.
Large orders: 98% on - time delivery for 100,000 - unit orders, thanks to lean production scheduling.
This agility matches your business expansion, whether you’re testing new markets or scaling up globally.